- E-mail: yqkexin@gmail.com
-
Kexin Global


Induction Weld Preheating: Process, Applications and Equipment Selection
Discover the induction weld preheating process. Learn about its applications, key benefits over flame heating, and how to select equipment for precise preheat & interpass temperature control.
August 05, 2026
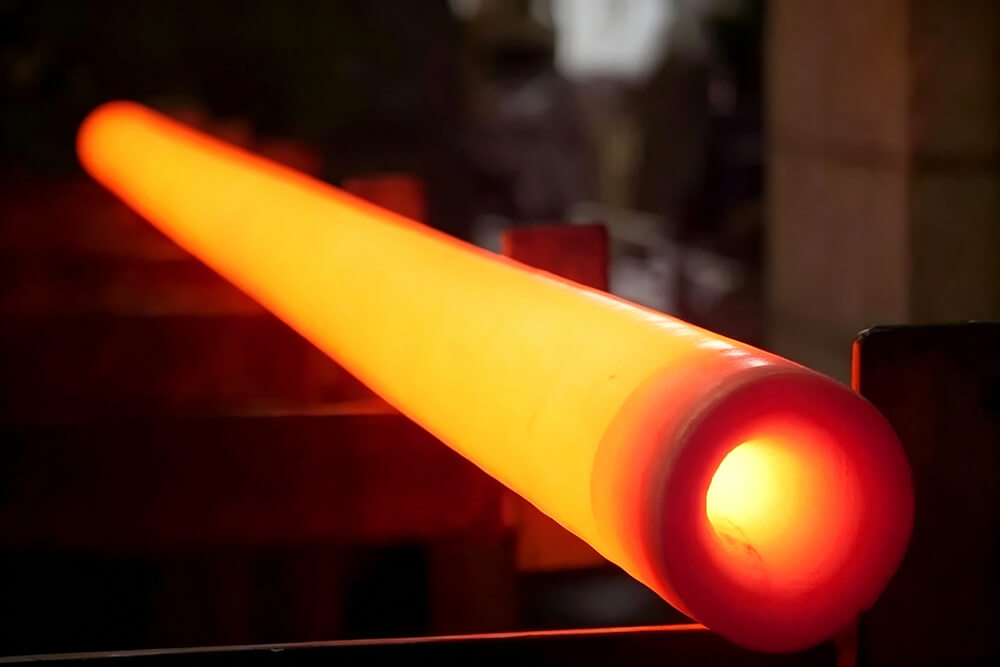
Some steels can be welded with little or no preheating, while thick sections, higher-carbon steels, and certain alloys require closer temperature control. Rapid cooling, hydrogen, and residual stress can increase the risk of cracking, making preheating an important part of many welding procedures.
Preheating raises the temperature around the weld area before welding begins, helping to slow the cooling rate and reduce temperature differences through the joint. The required temperature depends on the material, section thickness, and welding procedure.
Flame and electrical resistance heating are established preheating methods. Induction offers another approach, using an electromagnetic field to heat the workpiece directly and provide controlled, repeatable heating without an open flame.
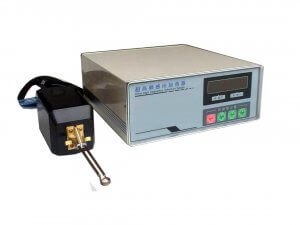
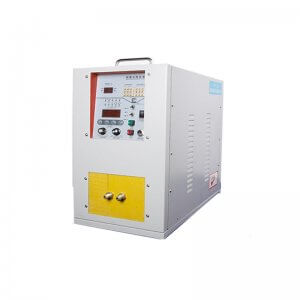
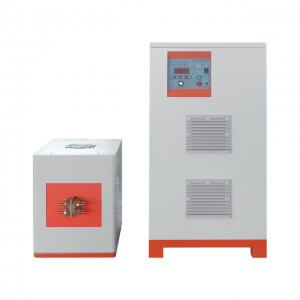
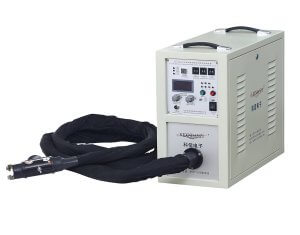
KEXIN supplies induction heating systems for weld preheating and other industrial heating applications. This article explains how induction weld preheating works, where it is used, and how it compares with conventional methods.

Why Preheating Matters in Welding
Preheating is done to control the cooling rate of a weld. When a weld is made, the weld metal and the heat-affected zone around it heat up, then cool back down. How fast they cool determines the final properties of the joint.
If the joint cools too fast, rapid contraction and hardening can pull the metal apart as it shrinks, leading to severe cracking.
Fast cooling traps hydrogen in the weld, allowing it to diffuse into the steel and make the joint brittle.
Hard, brittle zones can form rapidly in a fast-cooling heat-affected zone, compromising structural integrity.
Preheating slows the cooling rate. By starting with a warm base metal, the weld and the surrounding zone cool more gradually, which lets the microstructure form without cracks and drives out trapped hydrogen.
The need for preheat grows with the carbon content and the section thickness. High-carbon and alloy steels require higher preheat temperatures, and heavy sections lose heat faster, dictating a need for more intense preheat.
Induction Preheating vs. Flame and Resistive Blankets
Preheating has been done with oxy-fuel torches and electric resistive blankets for decades, and both still work. However, induction significantly changes the economics and efficiency for specific jobs.
| Preheating Method | Heat Zone | Speed | Temperature Control | Best Suited To |
|---|---|---|---|---|
| Induction | Targeted, even | Fast | Precise, repeatable | Pipe, heavy section, controlled preheat |
| Oxy-fuel flame | Broad, uneven | Slow | Poor | Field repairs, small joints, no equipment |
| Resistive blanket | Surface, large area | Slow | Moderate | Flat plate, large tanks, long soak |
The biggest advantage of induction preheating is that it heats the workpiece itself, evenly, without a fierce open flame on the surface. A flame can overheat the surface while the core stays cold, and it consumes a lot of fuel over an extended period. Induction delivers the heat exactly where the weld needs it, in minutes, with a controlled target temperature.
The second advantage is control. Induction hits and holds a precise preheat temperature, matching the exact requirements of the welding procedure. Repeatable control means every joint gets the same preheat, resulting in consistent weld quality and fewer rejects.
The third is safety and cleanliness. Induction produces no open flame, no fumes, and no soot, making it significantly safer around the weld zone and cleaner for the operator.
How Induction Preheating Works
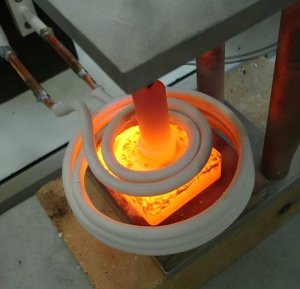
Induction preheating utilizes the same physics as all induction heating. A coil is placed around or against the weld zone, positioned close to the work piece without actually touching it. Alternating current running through the coil generates a powerful electromagnetic field, which induces eddy currents directly in the steel.
The natural electrical resistance of the metal turns those currents into heat. As a result, the steel warms from within, specifically near the surface where the weld will be made.
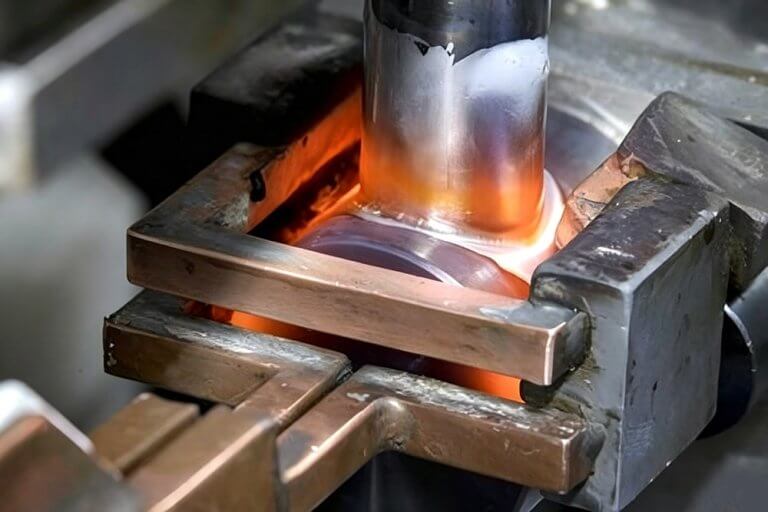
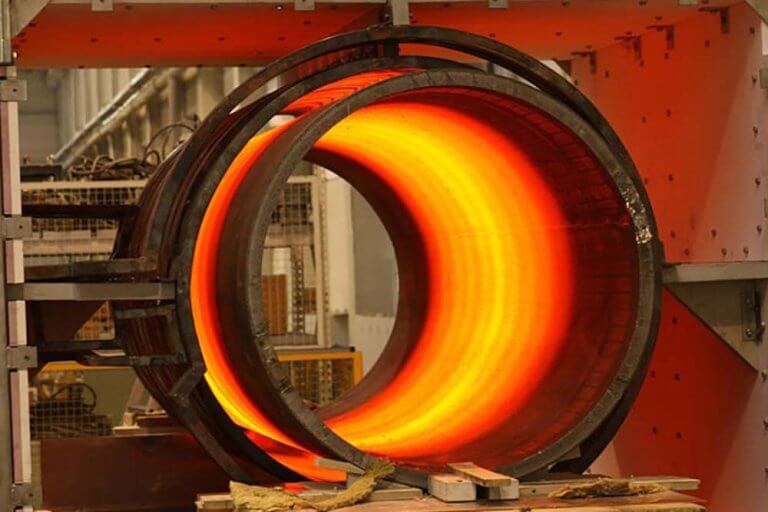
The coil’s shape directly defines the heated zone. A coil wrapped around a pipe heats the full circumference of the joint, ensuring an even preheat all the way around. Alternatively, a flat coil laid against a plate heats the weld area on one face. The operator simply positions the coil and sets the target temperature on the power supply; the system autonomously heats and holds the set point.
The operator then welds while the part remains at the preheat temperature. In some procedures, the induction system is also kept running to maintain the interpass temperature between multiple weld passes.
Common Applications of Induction Weld Preheating
Induction preheating is highly effective wherever a welding procedure demands controlled heat on heavy or alloy steels.
-
Pipeline Welding
Uses induction to preheat pipe ends to the specified temperature before roots and hot passes, guaranteeing even heat around the full circumference. -
Heavy Fabrication
Preheats thick metal plates before welding to prevent severe cracking in the root of multi-pass welds. -
High-Carbon & Alloy Steel
Preheats parts that would otherwise easily crack upon cooling, such as rails, hardfacing components, and tool steel repairs. -
Tank & Pressure Vessels
Preheats structural seams before welding and effortlessly maintains the interpass temperature on thick-wall vessels. -
Structural Steel Repair
Preheats cracked sections thoroughly to ensure the new repair weld does not re-crack under stress.
In every application, the core benefit remains the same: a weld that cools slowly enough to stay structurally sound, executed with highly repeatable control.
Controlling Preheat and Interpass Temperature
Weld preheat is strictly specified by the welding procedure, and hitting those exact numbers is what makes the joint hold.
Preheat temperature is the minimum temperature the base metal must reach before any welding starts. Heat too little, and the joint cools too fast. The welding procedure clearly states the required temperature, and the preheat must reach it evenly across the entire weld zone.
Interpass temperature is the temperature maintained between weld passes on a multi-pass joint. Keeping the joint above the minimum temperature while it is being built ensures every pass lays on a sound base, effectively avoiding cracking between passes.
Induction controls both parameters flawlessly. The power supply reads the part’s actual temperature and holds it at the precise set point, allowing the operator to work at a stable temperature instead of constantly chasing a cooling part with a manual torch.
The Role of Temperature Monitoring
Reliable preheat absolutely depends on knowing the real temperature of the workpiece. A common and dangerous mistake is relying on the torch size or the operator’s personal experience instead of actually measuring the metal. Induction systems solve this by utilizing a temperature sensor or a controlled heating profile to scientifically confirm the part has reached the target before welding ever starts.
Accurate measurement matters because underheating inevitably produces a cracked joint, and overheating can severely damage the material’s properties. A controlled induction system completely removes the guesswork, guaranteeing the weld is made at the exact temperature the procedure specifies.

What to Consider When Selecting an Induction Preheating System
The right induction preheating system depends heavily on the workpiece and the specific welding procedure. Part size, target preheat temperature, and required heating time all directly influence the total power needed. A large-diameter pipe or a very thick section, for example, will generally require significantly more heating capacity than a smaller component.
Coil design is just as important as raw power. The coil needs to perfectly suit the joint geometry and the exact area being heated; pipe applications may use coils arranged around the circumference, while plates and seams require a completely different configuration.
Temperature control capabilities should also exactly match the requirements of the welding procedure, including the specified preheat and acceptable interpass temperature ranges.
KEXIN supplies induction heating systems with application-specific coil design, professional installation support, and comprehensive technical training, allowing the equipment to be configured around your actual welding process rather than being selected on power rating alone.
Conclusion
Induction preheating offers a highly controlled and repeatable way to bring the weld area to the exact required temperature before welding begins. When correctly applied, it can help carefully manage cooling rates, support incredibly consistent weld quality, and drastically reduce reliance on inefficient open-flame heating.
The chosen system should always be matched to the actual welding procedure rather than selected on output power alone. Material type, section thickness, joint geometry, target preheat and interpass temperatures, and daily production requirements all heavily influence the ideal equipment and coil configuration.
FAQs
Related Articles
Explore News >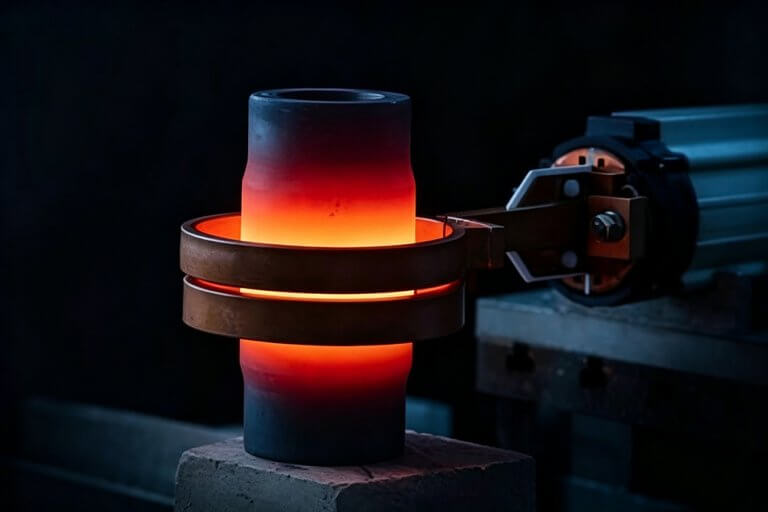
Request A Quote
Can't find the answer you need? Tell us about your application and our engineers will get back to you.